Selecting Conveyor Equipment Manufacturers for Regulated Industries
07/17/2026
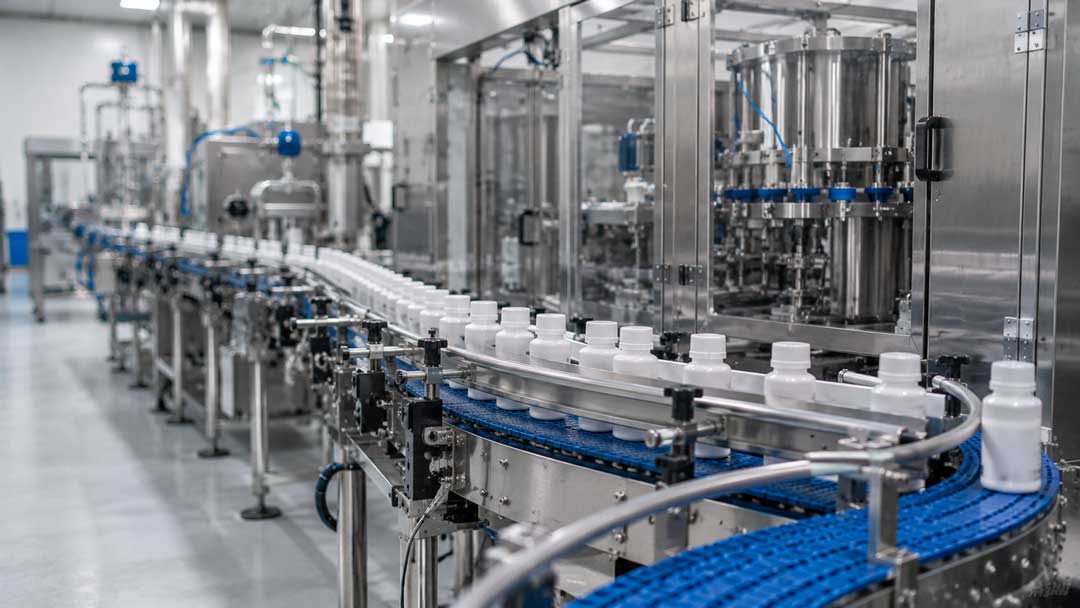
Choosing the right conveyor equipment manufacturer plays an important role in production efficiency, product quality, and long-term operational performance. Whether you are expanding an existing production line or installing new Packaging Equipment, selecting an experienced engineering partner helps ensure your system supports your production goals while integrating smoothly with existing equipment.
Manufacturers serving regulated industries must design equipment around facility layouts, sanitation requirements, throughput objectives, and future production growth. Custom engineering, responsive technical support, and dependable system integration all contribute to equipment that delivers reliable performance throughout its service life.
Local Experience and Industry Reputation
When evaluating conveyor equipment manufacturers, experience and customer satisfaction provide valuable insight into long-term performance. Manufacturers with a history of serving regulated industries understand the practical challenges that production facilities face every day.
Our experience designing conveyor systems for packaging allows us to support facilities across food and beverage, pharmaceuticals, nutraceuticals, cosmetics, meat processing, spices, and cannabis production. Every project begins with understanding production goals, facility layouts, and integration requirements before equipment is designed.
Customer relationships built through reliable engineering, responsive service, and long-term support often provide a stronger measure of performance than marketing materials alone.
Product Range Designed for Packaging Applications
A complete packaging line depends on equipment that works together efficiently from product filling through final packaging. We engineer integrated Packaging Equipment that supports smooth product movement across every stage of production.
- Conveyor Systems: Our Conveyor Systems transport bottles, containers, cartons, trays, and pouches while supporting efficient product flow throughout the packaging process. Stainless steel construction and modular designs simplify cleaning and maintenance in regulated production environments.
- Liquid Filling Equipment: Our Liquid Filling Equipment integrates with upstream and downstream systems to help maintain consistent production while accommodating different container sizes and product formats.
- Rotary Equipment: Rotary Equipment provides efficient product accumulation and transfer between production stages. Modular stainless steel construction allows these systems to integrate easily into facilities with varying floorplans and production layouts.
- Capper Machine Integration: Our Conveyor Systems are engineered to work seamlessly with Capper Machine installations, supporting efficient product handling throughout the packaging line.
By designing complete production systems, we help manufacturers create packaging lines that remain adaptable as production requirements evolve.
Customization Capabilities for Unique Operations
Every production facility has unique requirements. Rather than offering standardized equipment for every application, we engineer Conveyor Systems around each customer's operational goals.
- Facility-Specific Engineering: We design systems that accommodate available floor space, product flow requirements, and production objectives while supporting efficient line layouts.
- Modular Equipment Design: Modular Conveyor Systems and Rotary Equipment simplify future expansion, maintenance, and production line modifications without requiring complete system replacement.
- Stainless Steel Construction: We manufacture equipment using stainless steel where appropriate to support sanitation, durability, and simplified maintenance in regulated industries.
- Integrated Packaging Lines: Our Conveyor Systems are engineered to integrate with Liquid Filling Equipment, Rotary Equipment, induction sealers, labeling equipment, Bottomless Side Belt Transfers, and Capper Machine systems for efficient production flow.
This application-focused approach helps manufacturers build production lines that support both current and future operational requirements.
Engineering Support Throughout the Equipment Lifecycle
Selecting Conveyor Systems extends beyond equipment design. Ongoing engineering support contributes to reliable operation and long-term production performance.
- Project Planning: Our engineering team works with customers throughout system design and equipment selection to develop solutions aligned with production goals.
- Technical Support: We provide continued technical assistance following installation to help facilities maintain consistent equipment performance.
- Replacement Components: Access to replacement parts and modular system upgrades helps support routine maintenance while preparing production lines for future expansion.
Working closely with customers throughout the equipment lifecycle allows production teams to maximize the value of their Packaging Equipment investment.
Production Scheduling and Delivery Planning
Project timelines are an important consideration when selecting conveyor equipment manufacturers. Production schedules often depend on careful coordination between engineering, manufacturing, installation, and equipment integration. Standard Conveyor Systems may be available more quickly than highly customized production lines, while engineered solutions require additional design and manufacturing time to ensure proper integration with existing equipment.
Because every project differs, we work closely with customers during the planning stage to establish realistic production schedules that align with installation requirements and operational objectives.
Compliance with Industry Standards
Compliance remains a critical consideration for manufacturers operating in regulated industries. Equipment should be designed with sanitation, reliability, and long-term operational consistency in mind.
- UL-Certified Components: We incorporate UL-certified electrical components to support dependable system integration and reliable equipment performance.
- Sanitary Equipment Design: Stainless steel construction supports efficient cleaning and maintenance in food, pharmaceutical, nutraceutical, cosmetic, and other regulated production environments.
- FDA, USDA, and GMP Considerations: When appropriate for the application, our Conveyor Systems are designed to support facilities operating under FDA, USDA, and GMP guidelines.
- Engineering Review: Every project includes careful evaluation of facility requirements to help ensure equipment integrates effectively within existing production processes.
These engineering principles support production environments where consistency, sanitation, and equipment reliability remain priorities.
Installation Support, Training, and Technical Assistance
Successful equipment installation continues beyond startup. Proper training helps production teams operate Conveyor Systems efficiently while simplifying routine maintenance and production changeovers. Our engineers provide installation guidance, operator training, maintenance recommendations, and technical assistance to help facilities maximize equipment performance throughout its service life.
As production requirements evolve, we continue working with customers to support production line modifications, equipment additions, and future Packaging Equipment integration projects.
With more than 15 years of experience and a dedicated manufacturing facility in Miami, GLOBALTEK® engineers and manufactures Conveyor Systems designed for performance, sanitation, compliance, and long-term reliability.
Whether you are installing a new production line or expanding an existing operation, we work with you to deliver Conveyor Systems that align with your facility layout, production objectives, and long-term operational goals.
Comments
No posts found