How Heat Induction Sealers Improve Product Shelf Life
04/25/2025
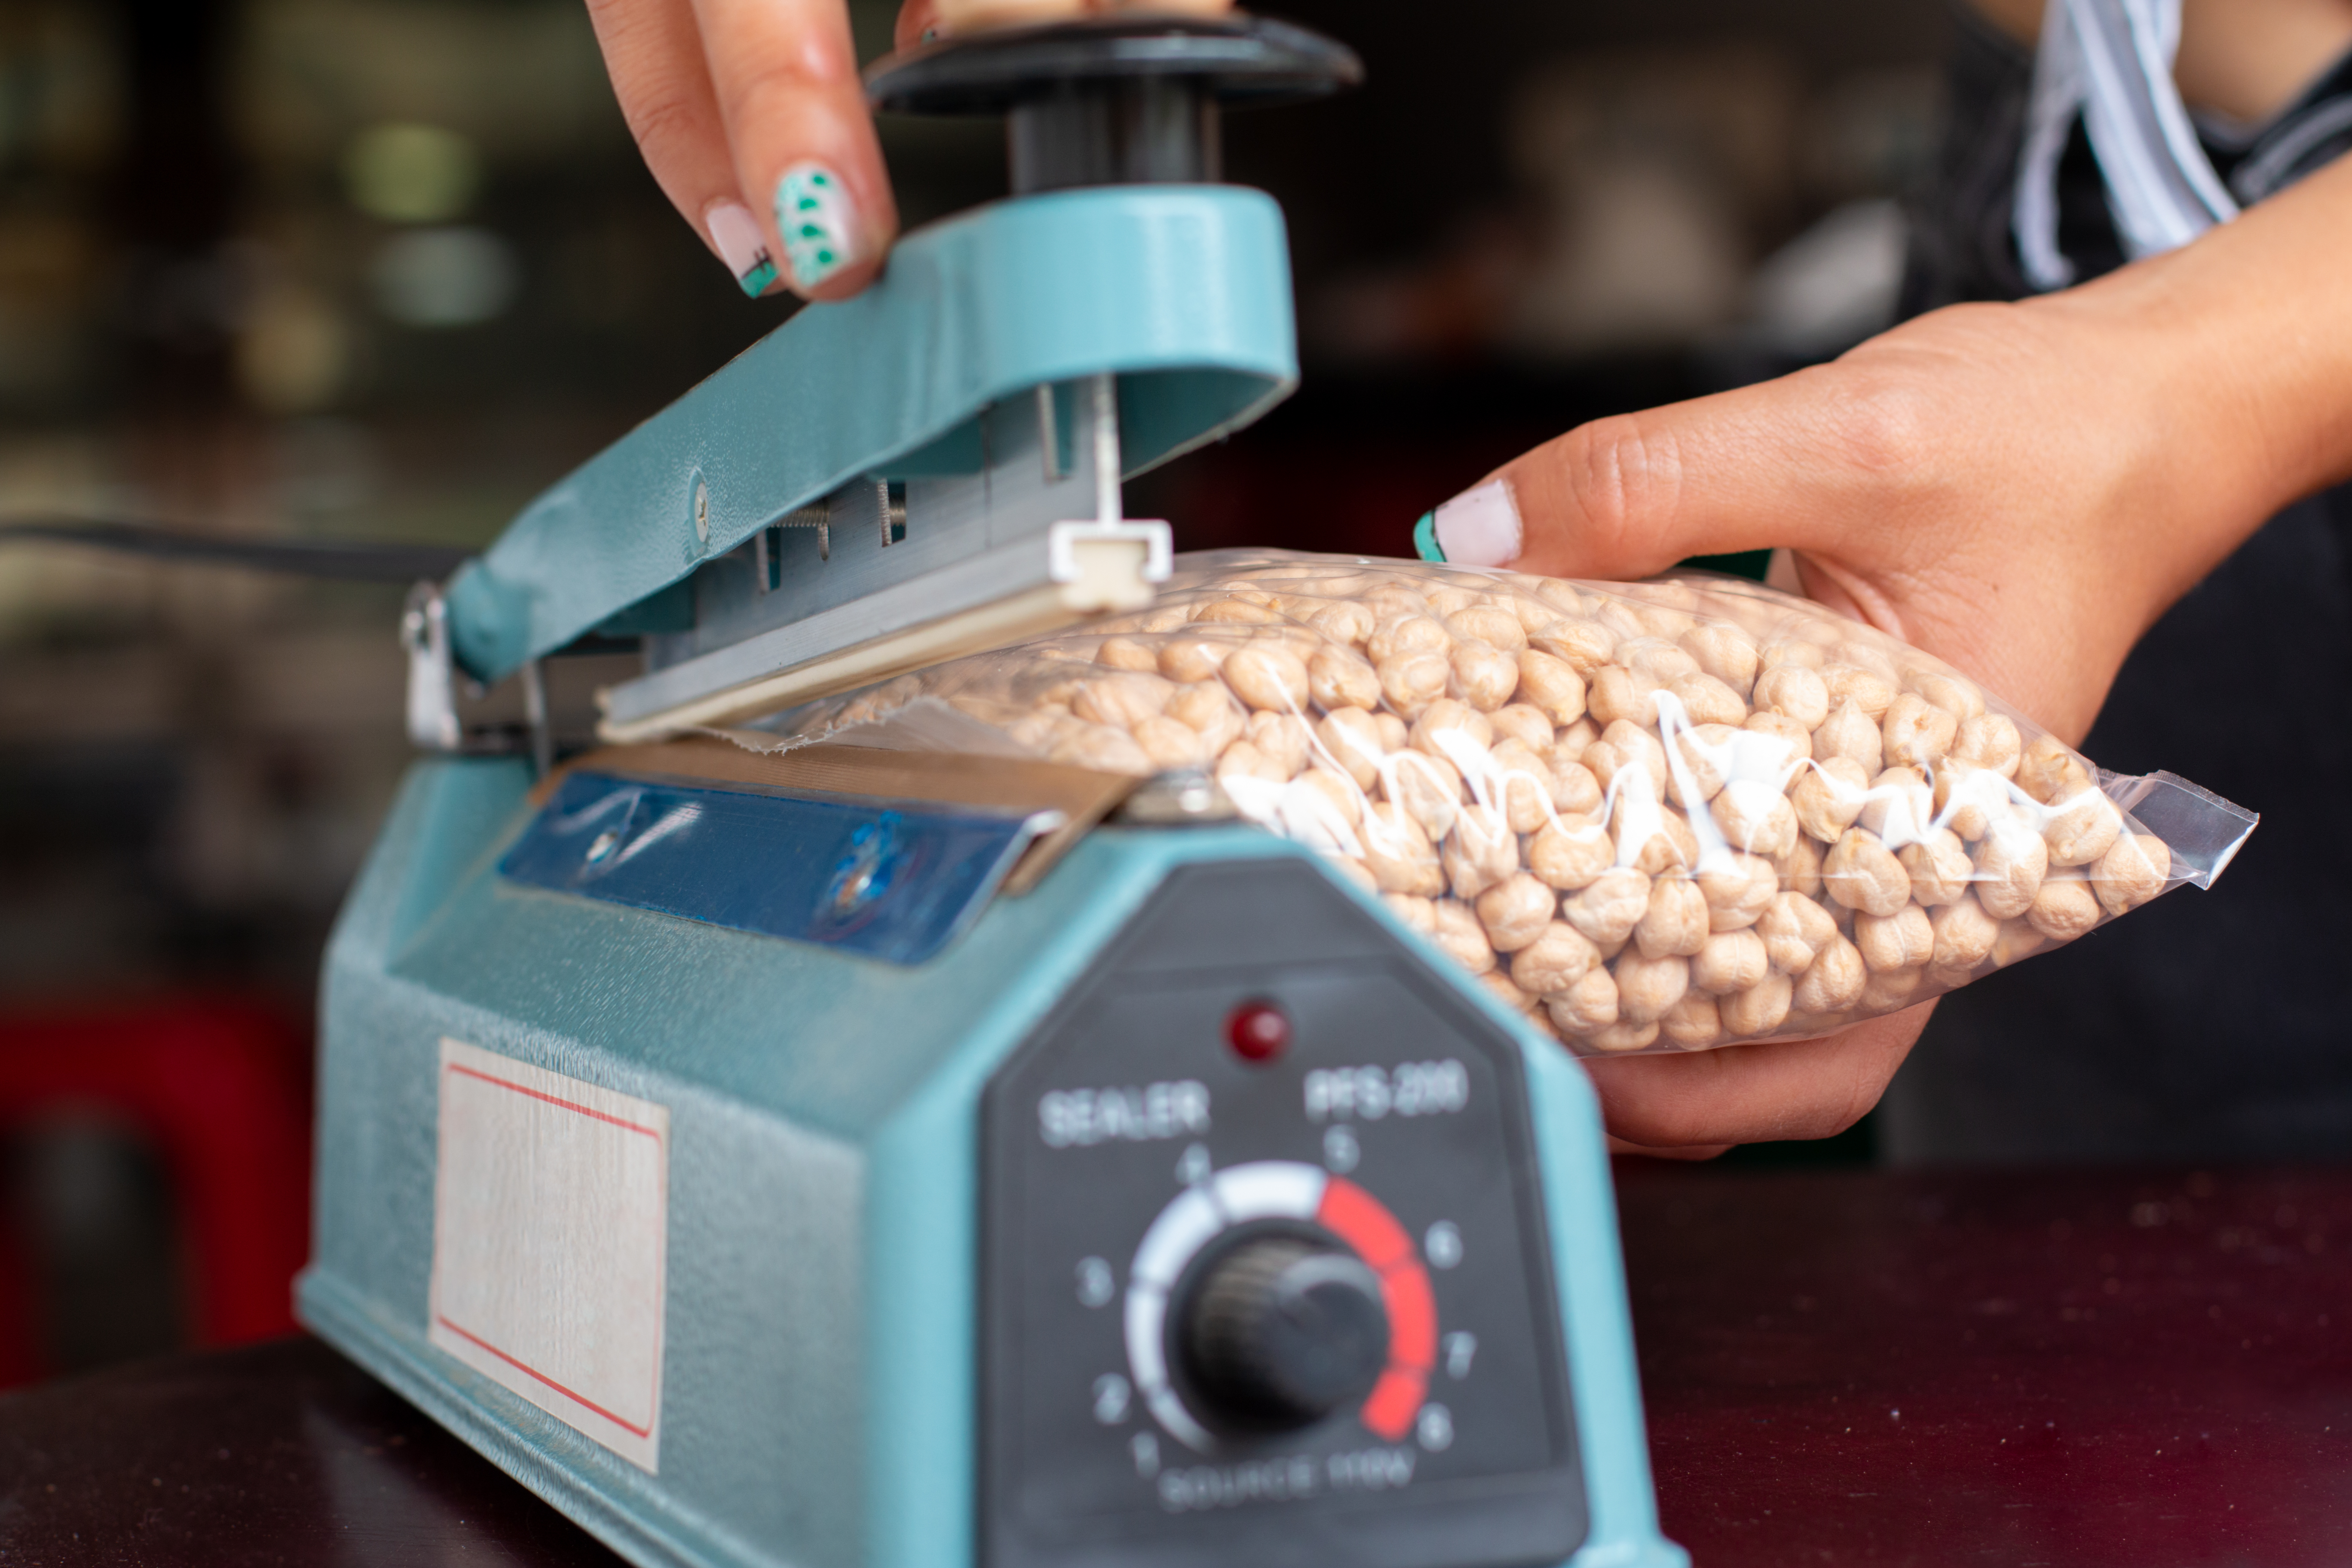
Product freshness and safety depend heavily on proper packaging. Heat induction sealers do the trick. Reliable and efficient, the machines seal containers to preserve freshness. Imagine: Airtight seals on your plastic and glass, extending the life of your food. Consumers and the product itself both win with this streamlined process.
Interested in learning the mechanics? Heat induction sealers use hot induction heads to fuse layers of paper pulp, aluminum, and wax liners to the container, forming a secure barrier that keeps out moisture, oxygen, and contaminants. The FDA's tamper-evident rules are met by our process. No leaks, no damage, just happy customers!
Reducing waste is a nice side benefit; fewer extra closures are needed with this sealing technique. First, let's discuss the benefits of heat sealing. Its ability to stop contamination is a big one.
How Heat Sealing Prevents Contamination
Here’s what happens: a protective liner is fused to the container using controlled heat. That simple step creates a seal that blocks out dust, bacteria, and anything else that might compromise your product. According to Section 6 of the Packaging Systems guidelines, these seals are far more tamper-resistant than adhesive-only options.
If you’re packaging hazardous or sensitive contents, you’ll appreciate how strong the bond is. Heat seals don’t loosen under pressure, and because you’re using thermal energy instead of heavier mechanical closures, you end up using less material, which means less waste.
You also get the benefit of faster packaging on conveyor lines, since the process is streamlined and highly compatible with automated systems. Once sealed, your containers are locked tight, protecting quality and safety from start to finish.
Enhancing Product Freshness with Airtight Packaging
Keeping your products fresh isn’t just about storing them in the right place; it starts with the right seal.
- Preserving Flavor: An airtight seal helps trap essential flavor molecules, preventing outside air from dulling your product’s taste. In fact, studies show up to 30% less spoilage with induction sealing. Whether you’re packaging spices, sauces, or snacks, flavor stays consistent from the production line to the consumer’s home.
- Maintaining Texture: Moisture is the enemy of crunch. With an effective heat seal, cereals stay crispy, chips don’t go stale, and customers enjoy that satisfying texture you worked so hard to create. The sealed barrier keeps the structure intact and makes for a better experience with every bite.
- Protecting Nutrients: Sealing in freshness also means sealing in nutrition. Airtight packaging reduces oxygen exposure, which helps retain vitamins and nutrients. Research shows this can cut nutrient loss by 25%, helping your products deliver more value (and more health benefits) to your customers.
Extending Shelf Life Through Tamper Evidence
When customers see a tamper-evident seal, they know they’re getting a safe, untouched product. That builds trust, and trust leads to loyalty.
- Secure Barriers: Heat induction creates strong, reliable seals that bond liners directly to glass or plastic. This meets FDA requirements for tamper-evident packaging, ensuring each container is safe from tampering and clearly protected.
- FDA Validation: Section 6 of the FDA packaging rules confirms that induction sealing outperforms adhesives when it comes to preventing breaches. When shoppers see your packaging, they feel reassured, which reflects positively on your brand.
- Longer Shelf Life: Tamper-proof seals also help your product last longer. By blocking contaminants and stabilizing internal conditions, the seal maintains quality and freshness well beyond standard shelf life.
The Role of Induction in Preserving Quality
If you’re aiming for consistency and performance across every unit, heat induction is your friend.
It works by generating an electromagnetic field that heats the cap’s foil liner. As the wax melts, it fuses the paperboard to the aluminum layer, creating a tight, uniform bond. This bond keeps your product safe and stable throughout its shelf life.
Different container sizes require different tools:
- Containers up to 53mm often use a tunnel sealing head
- Larger sizes may benefit from a flat sealing head
Either way, both options deliver strong closures that minimize product failures.
These systems are especially common in the food and personal care industries, where quality control is critical. Thanks to the dependable seal created by the wax, foil, and polymer, your brand earns a reputation for reliability.
Improved Protection Against Moisture and Oxygen
One of the biggest threats to product integrity? Moisture and air. Induction sealing offers solid protection against both.
With this method, you keep water and oxygen out of the container, which helps preserve texture, color, and flavor. That also means you lower the risk of mold, spoilage, and nutrient breakdown, which translates into fewer complaints and returns.
By investing in a hermetic seal, you’re also investing in consumer satisfaction. Shoppers get more consistent quality and shelf appeal, and you protect your bottom line from waste and rework.
Minimizing Leakage Risks with Secure Closures
Shipping and storage can be rough on packaging. Induction sealing ensures your products stay sealed and your reputation stays intact.
- Sealed Barriers: A heat-sealed container won’t leak or spill during transport. That’s a win for your supply chain and your customers, who will appreciate the clean, tamper-proof experience.
- Boosted Consumer Confidence: When customers see an intact seal, they know the product hasn’t been touched. This visible protection reassures buyers and encourages repeat purchases.
- Reduced Product Losses: Leaky containers lead to mess, returns, and lost revenue. A solid heat seal reduces these risks with proven bonding technology that holds up across shipping environments.
Boosting Brand Trust via Advanced Packaging
The benefits of induction sealing go beyond just product protection; it also improves how customers perceive your brand.
- Trust Growth: Surveys show that over 70% of consumers prefer tamper-evident packaging. A crisp, secure seal boosts confidence and increases customer loyalty over time.
- Refined Presentation: Clean, sealed packaging looks professional and high-end. In competitive retail spaces, that polished look helps you stand out. A 2024 packaging trends report even noted growing demand for brands that prioritize security and appearance.
- Extended Partnerships: Retailers and distributors love working with brands that deliver consistently sealed, low-risk products. Fewer issues in transit mean more stable relationships and stronger shelf placement opportunities.
Heat induction sealers offer a reliable, efficient way to extend shelf life, preserve product quality, and improve customer trust. By applying a sealed foil or plastic layer, they block out contaminants and moisture, all while meeting the highest safety standards.
Studies even suggest that products using induction sealing can extend shelf life by up to 50%. That means more satisfied customers, better store reviews, and fewer returns.
Some store owners even mention how customers comment on the seal itself, which makes the product feel safer and fresher. Plus, with seamless operation on automated lines, these machines help you scale without slowing down.
So if you’re ready to reduce waste, boost freshness, and earn customer trust, heat induction sealing might be your smartest packaging move yet.
Comments
No posts found