How Florida Beverage Plants Vet Conveyor Manufacturers
09/10/2026
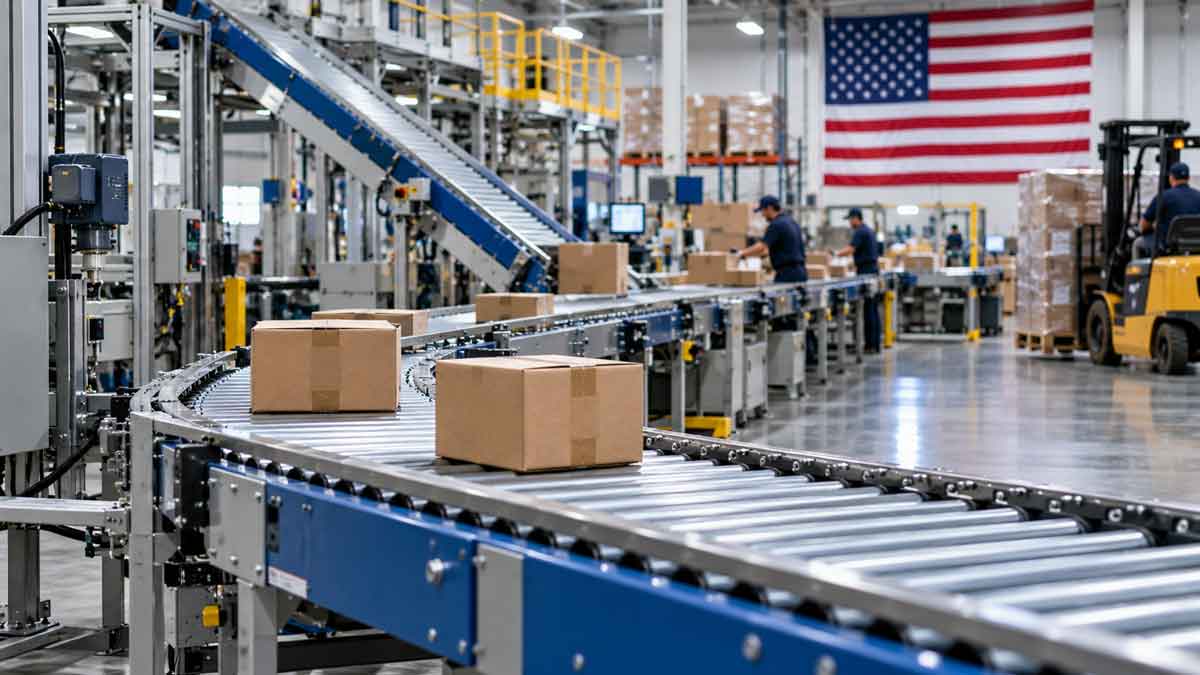
Florida beverage plants use a strict process when selecting conveyor equipment manufacturers. Local operations rely on packaging conveyor systems in the United States that are purpose-built for cleanliness, efficiency, and regulatory compliance. Plant managers weigh technical specifications against day-to-day maintenance needs to make sure production runs stay consistent under FDA oversight.
Many consider how each supplier's experience with Liquid Filling Equipment or Capper Machines aligns with evolving market demands and plant safety protocols. Firms often look at integration flexibility for Rotary Equipment within custom floor plans so automated systems work without bottlenecks or unplanned downtime.
Our ability to engineer scalable solutions while supporting long-term durability helps clients plan ahead rather than just buying hardware off the shelf.
That is why we start by looking closely at a manufacturer's track record and industry experience before making a commitment.
Evaluating Track Records and Industry Experience
Evaluating a conveyor supplier's track record means looking at more than its years in business. The right partner for Florida beverage plants has hands-on experience with packaging conveyor systems in the US.
Is there proof they have done projects with strict USDA or FDA rules? We always look for proof or client references that demonstrate successful installations in beverage plants like yours. Multiple installations reveal key lessons, including how even one conveyor breakdown can stop your line for hours.
How they address unplanned downtime, especially when conveyor systems become a single point of failure, tells you a great deal about their reliability. We recommend asking how they adapt to demanding, real-world conditions and handle service after installation.
Assessing Compliance with Food Safety Standards
Food safety rules are strict across beverage plants, and each conveyor system must meet stringent requirements. We make sure every GLOBALTEK® solution meets FDA, USDA, and Good Manufacturing Practice benchmarks before installation.
- Sanitary Build Assessment: We check whether your conveyor systems use stainless steel frames, smooth welds, and cleanable surfaces at all key touchpoints. This design helps cut the risk of bacterial growth by letting you do fast, deep cleaning after each production run.
- Verification of Certified Components: Our team checks that each conveyor system uses only UL-certified electrical parts and that liquid filling equipment, rotary equipment, and capper machines use food-grade materials. These steps help make sure your full line of packaging equipment is fit for beverage processing, with both compliance and performance in mind.
- Alignment with Preventive Controls: We look for automation features that support preventive controls under the Food Safety Modernization Act, such as belt enclosures and reduced product handling. When you limit human contact and reduce food exposure, you lower the risk of external contamination during operation.
Reviewing Customization and Integration Options
Customization and integration options shape how your Florida beverage plant's production line adapts to growth or new rules. A smooth fit with your current packaging equipment matters.
- Line Compatibility: Every conveyor must work with the fillers, cappers, and labelers already on the floor. Ready-to-link systems mean fewer hassles, quick installs, and no lost time when you hook up to line assets.
- Floorplan Flexibility: Plants often have tight footprints or unique production flows in Florida's beverage industry. You can configure conveyor systems around walls, corners, and wash zones, which helps boost throughput and reduce wasted space.
- Unified Controls: You want one control point for conveyor systems and rotary equipment. When you can link new and existing automation, you reduce training time and make operational errors less common.
Inspecting Durability and Maintenance Support
Assessing conveyor system durability and day-to-day maintenance support can often make or break plant operations. You want real proof that any line addition, whether it includes Packaging Equipment, Rotary Equipment, Liquid Filling Equipment, or a Capper Machine, will hold up in a high-washdown, high-use Florida facility.
- Durability means choosing conveyor systems built with stainless steel frames, sealed bearings, and parts that resist rust caused by daily sanitizer use and temperature swings. Our engineering teams spot belt stretch and modular joint wear in similar Florida beverage operations, and we address these issues during design to reduce stoppages.
- Maintenance support includes giving you access to written PM schedules, digital inspection logs, and clear work order tracking. We give you complete belt-material and chemical-compatibility specifications up front, so you can align service times with plant sanitation routines and ensure nothing gets missed between shifts.
- Fast part replacement is a must, especially during peak runs or seasonal shifts when downtime is costly. You get a dedicated national support line for GLOBALTEK® clients for fast troubleshooting and shipment of components, driving confidence in every service call.
Comparing Energy Efficiency and Sustainability
Comparing Conveyor Systems for energy use and sustainability will help you cut costs and curb environmental impact. High energy use and changing regulations have made this a top concern for Florida beverage makers.
- Energy Use Reduction: Modern Conveyor Systems built with energy-saving drives can cut total power use. This means lower monthly energy bills and less strain on your plant's power system.
- Sustainable Materials and Builds: When you choose Packaging Equipment with UL-certified stainless steel and recyclable parts, you can align with both current regulations and new ESG goals. Stainless steel lasts a long time, and you can clean it with ease, cut waste, and avoid costly swaps.
- Designed for Fewer Downtime Losses: Proven process upgrades can help you spot wasted energy, such as energy used when lines run during idle shifts or energy lost through leaks you can stop. Industry audits show that cutting leaks and tuning start-stop cycles can save thousands per year for large beverage facilities.
Checking Aftermarket Services and Warranties
Manufacturers know that strong aftermarket support is key to long-term uptime and trust in Conveyor Systems and Packaging Equipment. It is smart to check what happens after the install and how warranties fit into your risk plan.
- The warranty terms are more than a piece of paper. You get peace of mind when you know replacement parts, routine service, and on-site technical support are clearly spelled out from the start.
- Aftermarket services affect production downtime and total costs. When GLOBALTEK® offers readily available spare parts and fast-response engineering teams, you reduce production interruptions and avoid shipment delays.
- Support for Liquid Filling Equipment and Rotary Equipment goes beyond routine fixes. If your operator calls with a problem, help should be fast and skilled so your team gets back to on-time output without any avoidable bottlenecks.
Analyzing Turnaround Times and Delivery Reliability
Once aftermarket services and warranties are reviewed, attention turns to turnaround times and delivery reliability for conveyor systems. Fast order fulfillment is not just a preference; it is essential for beverage producers on tight schedules. You start planning for each Packaging Equipment project with clear specs and drawings sent up front. Short feedback cycles speed things up and help keep your schedule on track. The impact of supply chain strength is real. The right Conveyor Systems partner will have steady in-house processes and quick access to common parts for faster shipping. Is your plant located in Florida? There are cases where location and vertical integration speed up shipments and cut risk. Florida beverage plants use a detailed process to vet conveyor manufacturers and ensure every system suits their needs. Quality Packaging Equipment always starts the conversation. We focus on evaluating how Conveyor Systems will adapt to existing floorplans. Reliable integration depends on matching Liquid Filling Equipment with high-speed Rotary Equipment. UL certification and Made in the USA components help minimize unexpected downtime. When clients look to expand, we provide floorplan-based solutions to optimize throughput and sanitary handling. Fast changeover and easy cleaning rank among the top reasons clients trust GLOBALTEK® systems. Clean design supports regulatory requirements and long service life. Each installation showcases the value of matching Capper Machines and filling systems with proper conveyors. Our support team prioritizes uptime, preventive service, and seamless automation. By choosing GLOBALTEK®, beverage plants invest in long-term partners with experience, reliability, and verified regulatory compliance.
Comments
No posts found