Curved Belt Conveyor ROI: Benchmarking Integration Success
04/23/2026
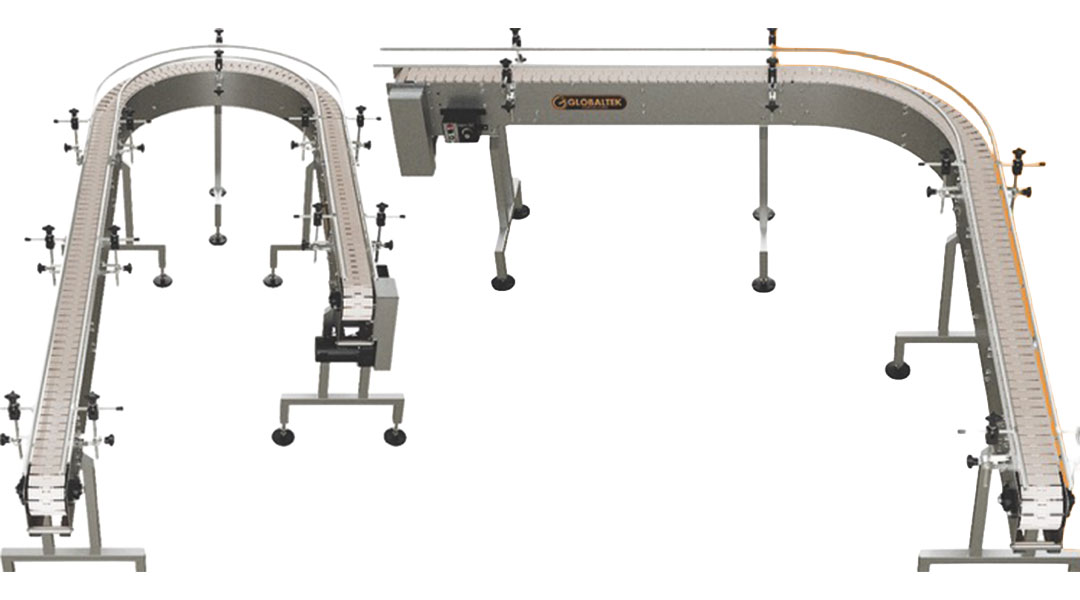
Curved belt conveyor systems in the USA offer a clear path to higher output. Many sites rely on these conveyors for tight space fit. They handle hard floorplans where straight-line movement isn't possible.
However, you need data to track how well new curved belt conveyor setups give you real value over time. Standard benchmarks focus on flow and uptime, but you should look deeper into full ROI math across your whole line.
Steady gains in speed, space use, and compliance can add up to clear savings for regulated fields like food or pharmaceuticals. To start with strong ROI benchmarking, sizing capex and opex for curved belt conveyor projects is key.
Assessing Capital and Operational Costs
Assessing up-front and running costs is vital for any curved belt conveyor systems in the USA integration. The first up-front cost for install may seem large, often between $15,000 and $85,000, based on load size and layout.
However, many makers see long-term value when they invest in UL-certified, stainless steel builds that cut swap-out needs. Are you factoring in power use, belt swaps, and lube plans in your year-one budget plan?
The gap in running costs can hit 18% between old conveyors and new GLOBALTEK® models tuned for non-stop flow. In addition, you can also save on labor when your systems link with fillers and rotary gear on the same line.
A key point is how better wash-down features cut your cleaning labor and down time costs. The result is repeat running savings that back both performance and compliance.
Evaluating Labor Savings and Efficiency Gains
Labor savings and efficiency gains are two of the main factors driving curved belt conveyor ROI within automation. Careful benchmarking shows how these conveyor systems can cut repeat tasks and free up skilled operators.
- Streamlining Manual Handling: Adding curved belt conveyors will cut the need for you and your team to manually sort, push, or reposition product loads. This cuts fatigue and repeat strain, so you can focus on work that needs care and skill.
- Increasing Throughput Consistency: Products move smoothly and at set speeds, keeping steady output rates through each shift without bottlenecks or slowdowns. By keeping your line moving, curved conveyors support higher total volumes and faster order fulfillment.
- Reducing Staff Requirements Per Shift: With material handling automated by these conveyor systems, fewer people are required to keep each production area running during day-to-day use. This frees you up for other jobs and cuts overtime costs, offering clear labor savings over each month.
Analyzing Maintenance and Downtime Impacts
Maintenance and unplanned downtime directly affect production speed and long-term system value in curved belt conveyor projects. By looking into the most common downtime causes, you can find ways to boost both uptime and system ROI.
- Identifying Downtime Drivers: Studies by Guidewheel Performance Analysis show electrical and controls issues cause 92.9% of conveyor downtime in household goods sectors. A single event can stop work for over four hours, showing the need for strong part health checks.
- Cleaning and Changeovers: In food and beverage packaging, median conveyor runtime drops to 36.1% due to needed cleaning and frequent changeovers. These pauses are planned but still cut total output, showing the value of conveyors made for faster, tool-less upkeep.
- Tracking Micro-Stops: Micro-stops lasting less than two minutes often slip past your manual logs but lower overall equipment effectiveness (OEE) if you don't manage them. Auto tracking helps you react faster with your maintenance teams, cutting total losses and helping you run smoother shifts.
Selecting the right curved belt conveyor will shape your line's ROI. Our GLOBALTEK® team has helped you and teams nationwide see faster setup and smoother product flow. Quick install and UL-certified design boost uptime and keep output high. Each conveyor is built in the United States for long-term use, easy cleaning, and a fit to your layout. As a result, you can cut bottlenecks and meet FDA and USDA rules with less labor. Our integration benchmarks show your new layouts can save as much as 30% in floor space. Systems like these give you more output with fewer manual steps. GLOBALTEK® packaging gear comes made to your specs, so your conveyors link with fillers, cappers, and rotary gear. This way, you get steady product flow and faster changeovers. Teams using our gear report fewer stops and longer service gaps, protecting both yield and what you invest. Reach out to see how GLOBALTEK® integration helps your facility meet strict needs while giving you long-term value.
Comments
No posts found