Choosing Conveyor Equipment Manufacturers: Key Attributes That Matter
07/16/2026
Selecting the right conveyor equipment manufacturer means weighing several factors that affect production efficiency, system integration, and long-term performance. The right partner delivers reliable Packaging Equipment designed to support regulated industries and high-volume production environments.
Whether you operate in food and beverage, pharmaceuticals, nutraceuticals, cosmetics, or cannabis manufacturing, your conveyor solution should align with your facility layout, production goals, and compliance requirements. Working with an experienced manufacturer also helps ensure your equipment integrates smoothly with the rest of your packaging line.
Proven Track Record in Packaging Solutions
When evaluating conveyor equipment manufacturers, one of the first qualities to consider is a proven history of designing dependable conveyor systems for packaging. Manufacturers with experience across regulated industries understand how production requirements vary and how equipment must adapt to changing product formats and packaging demands.
We engineer Conveyor Systems that support efficient product flow while integrating seamlessly with Liquid Filling Equipment, Rotary Equipment, Capper Machine systems, and other Packaging Equipment throughout the production line. Modular designs also provide greater flexibility when production needs evolve, helping facilities accommodate new packaging formats with minimal disruption.
For operations where sanitation, efficiency, and compliance are priorities, selecting conveyor systems for packaging that are built for long-term reliability helps support consistent production while maintaining product quality.
Advanced Customization Capabilities
Customization plays an important role in selecting Conveyor Systems that match your production environment. Rather than relying on one-size-fits-all equipment, we engineer systems around your operational requirements.
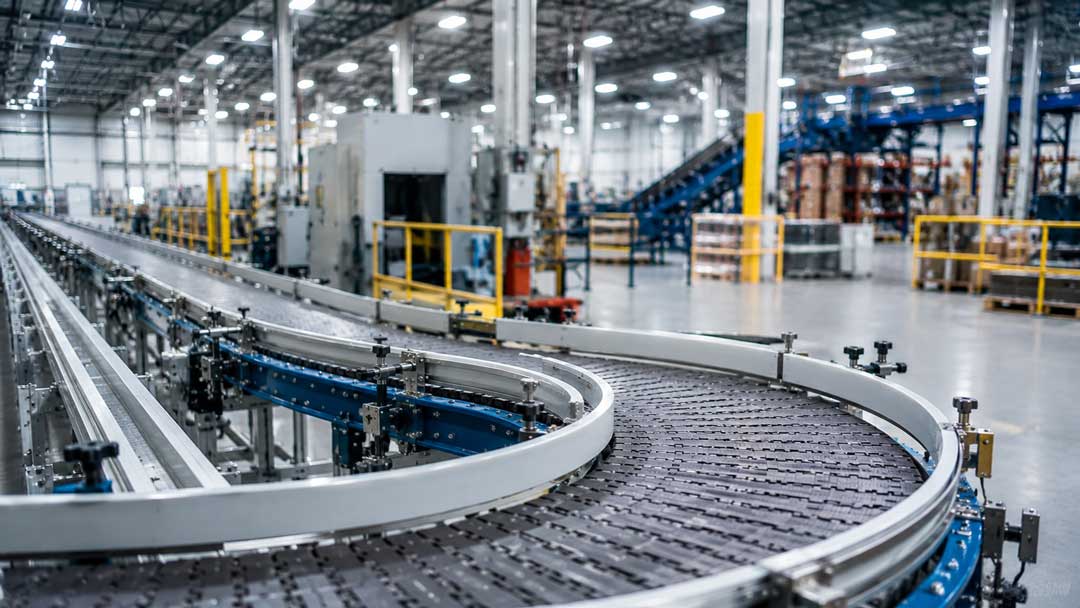
- Floorplan Adaptability: Every facility presents unique space considerations. We design straight and curved Conveyor Systems with custom transfer points and layouts that maximize available floor space while supporting efficient product flow.
- Production Flexibility: Different products require different conveying speeds and handling methods. Adjustable guides and configurable conveyor layouts allow equipment to support multiple production runs while simplifying changeovers.
- Compliance-Focused Design: Regulated industries require equipment built with sanitation and reliability in mind. We manufacture stainless steel Conveyor Systems using UL-certified electrical components and washdown-ready designs where appropriate to support food, pharmaceutical, nutraceutical, and cosmetic production environments.
By tailoring each system to production requirements, we help manufacturers improve line integration while supporting long-term operational performance.
Strong Regional Service Support
Responsive technical support remains an important consideration when selecting conveyor equipment manufacturers. Working with a manufacturer that offers engineering expertise before, during, and after installation helps keep production running efficiently.
- Responsive Technical Assistance: Headquartered in Miami, Florida, we support customers throughout the United States with experienced technical guidance for Conveyor Systems, Rotary Equipment, Liquid Filling Equipment, and Capper Machine installations.
- Replacement Parts and System Upgrades: We maintain access to UL-certified components and modular replacement parts that help simplify maintenance and support future production expansion.
- On-Site Training: Our engineering team provides installation assistance, operator training, maintenance guidance, and changeover support so your team can operate equipment confidently and efficiently.
This collaborative approach helps maximize equipment performance throughout its service life.
Integration-Ready Automation Solutions
Modern production lines depend on equipment that works together efficiently. Rather than operating as standalone machines, today's Packaging Equipment is designed to integrate across the entire production process.
We engineer Conveyor Systems that connect smoothly with Rotary Equipment, Liquid Filling Equipment, Capper Machine systems, induction sealers, labeling equipment, and other packaging line components. This integrated approach helps maintain consistent product flow while supporting production efficiency and simplified line management.
Modular system architecture also allows manufacturers to expand or reconfigure production lines as operational requirements change, providing long-term flexibility without replacing the entire conveying system.
Energy-Efficient Conveyor Designs
Energy efficiency continues to be an important consideration for manufacturers seeking long-term operational value. Well-designed Conveyor Systems can support efficient production while reducing unnecessary energy consumption through thoughtful engineering.
- Efficient Drive Systems: Proper motor selection helps match conveyor performance to production requirements while supporting consistent operation.
- Optimized Conveyor Components: Low-friction materials, quality bearings, and properly engineered belt systems contribute to smooth product movement and reduced wear over time.
- Simplified Maintenance Access: Equipment designed for routine inspection and maintenance helps maintain consistent conveyor performance while supporting long service life.
These engineering considerations contribute to reliable operation while helping manufacturers optimize day-to-day production.
Compliance with Industry Standards
For regulated industries, compliance is an essential part of equipment selection. Conveyor equipment manufacturers should demonstrate a clear understanding of applicable industry requirements without overstating certifications or capabilities.
- UL-Certified Components: We incorporate UL-certified electrical components throughout our equipment to support reliable system integration and electrical safety.
- Sanitary Equipment Design: Our stainless steel Packaging Equipment is engineered to support production environments where cleanliness and efficient maintenance are priorities.
- FDA, USDA, and GMP Considerations: When appropriate for the application, we design Conveyor Systems that support facilities operating under FDA, USDA, and GMP guidelines.
- Built for Regulated Industries: Our solutions are engineered for food and beverage, pharmaceuticals, nutraceuticals, cosmetics, meat processing, spices, and cannabis production environments where dependable equipment performance is essential.
These design principles help manufacturers build production lines that support operational consistency while meeting industry expectations.
Comprehensive After-Sales Support
Long-term support is another important factor when comparing conveyor equipment manufacturers. Equipment performs best when backed by experienced engineering assistance throughout its operating life. Our relationship with customers extends beyond installation. We continue supporting production teams with maintenance guidance, replacement components, technical assistance, and recommendations for future system expansion as production requirements evolve.
Whether your facility is planning equipment upgrades, production line modifications, or additional Packaging Equipment integration, our engineering team works alongside your staff to help maintain efficient operations. With more than 15 years of experience and a dedicated manufacturing facility in Miami, GLOBALTEK® designs and manufactures Conveyor Systems that support performance, sanitation, compliance, and long-term reliability. Our Made in the USA equipment is engineered for seamless integration with Rotary Equipment, Liquid Filling Equipment, Capper Machine systems, Bottomless Side Belt Transfers, induction sealers, and other Packaging Equipment used throughout regulated industries.
By combining custom engineering, stainless steel construction, UL-certified components, and application-specific system design, we help manufacturers build production lines that are scalable, easy to maintain, and ready to support changing production demands. Whether you are installing a new production line or expanding an existing operation, we work with you to deliver Conveyor Systems that align with your facility layout, production objectives, and long-term operational goals.
Comments
No posts found